
Cutting Colour Rejection in Footwear Production: A Manufacturer's Guide
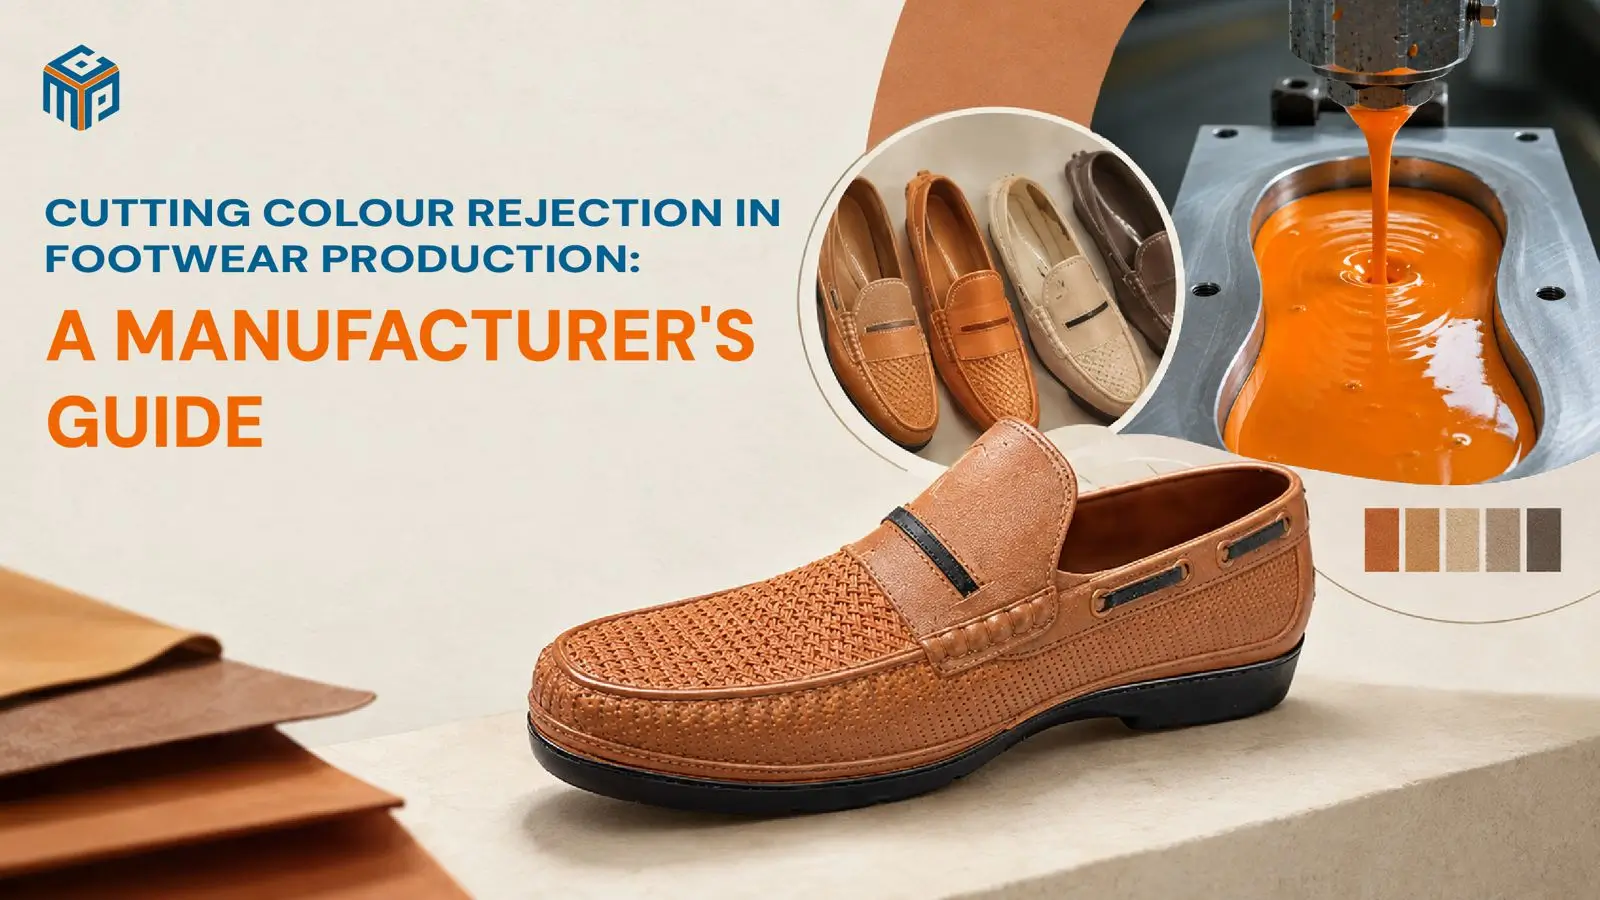
A footwear colour manufacturer sees the same complaint across most factories. An usual case of good soles going into the reject bin over a shade that is slightly off. The sole is structurally fine. It just does not match the required colour.
And to reduce the waste, along with the complaints, we need a deep dive. This guide walks you through where the ‘issue’ starts, what it costs and how to bring it down.
What Causes Colour Rejection in Footwear Production?
Three sources account for most rejected pairs.
Pigment lot variation: Pigment strength and diffusion can shift from one lot to the next, even from the same supplier. A paste that settles in the drum adds to this, since unstirred paste from the bottom carries more colour than paste from the top.
Dosing and mixing errors: Scooping paste by eye instead of weighing it is the most common cause on the floor. A short mixing cycle leaves pigment unevenly spread, which shows up as streaks or a patchy surface even when the dose was correct.
Mould temperature and substrate: Mould temperature changes gloss, and gloss changes how a shade reads. Sole density and thickness do the same. A shade approved on one mould can look different on another if these settings are not held constant.
How Much Does Colour Rejection Cost?
Cured PU cannot be recoloured, so a rejected sole is scrapped, downgraded or reworked at a lower price. That is the direct cost, and it is the smallest part of the problem.
The larger costs show up downstream. A rerun to replace rejected pairs pushes back your dispatch date. Mixed cartons slip through when left and right soles come from different runs, and a buyer catches it at inspection. Once a retailer spots a shade shift on the shelf, the next order is harder to win back.
How to Identify Where Rejection Starts
Pull the records before you change anything on the floor. Compare a rejected batch against an approved one: pigment lot number, dose, mixing time, mould temperature and sole density. Most factories skip this step and start adjusting the recipe instead, which only adds a new variable on top of the one causing the problem.
Change one factor at a time. If pigment, dose and mixing time are all altered together, you will fix the shade but never learn what was actually wrong.
How to Cut Colour Rejection: Step by Step
Standardise pigment and dosing. Buy from one pigment source and log the lot number against every batch. Stir the paste before each use, and weigh or meter every dose rather than estimating it.
Control mixing. Fix the mixing time and speed for each shade and keep it the same across every pour. A recipe is only as good as the step that applies it.
Inspect under a light booth. Judge colour under a single, controlled light source, not factory tube lighting. Two shades can look identical under one light and different under another, an effect called metamerism. Use a spectrophotometer where you can, since it reads colour as a number instead of leaving the call to whoever is standing at the line.
Re-match to the standard. Compare every batch against the approved physical sample, not against memory or the last pour. Keep that sample stored away from light so it does not fade and mislead your QC team.
How to Prevent Colour Rejection Before It Happens
Fixing a bad batch is slower than stopping one. A few habits keep rejection low over time:
- Write down the dose, mixing time and mould temperature for each approved shade, and route any change through QC rather than leaving it to an operator.
- Cast a small test piece from every new pigment lot and compare it against the last one before it reaches the floor.
- Keep a retained sample from every batch, so a complaint months later has something to check against.
- Review your rejection rate by shade, not just as one overall number. A single problem shade often skews the average.
For a deeper look at why batches drift once a recipe is locked, see our guide on colour batch consistency in footwear.
Why Footwear Manufacturers Choose Mittal Chemplast for Consistent Colour
Mittal Chemplast has worked as a footwear colour manufacturer since 1982. The Ansh range of PU colourants is built for footwear components, including soles, with lot-to-lot consistency as the starting point rather than an afterthought.
In-house formulation experts match shades to your sample and develop new formulas when the shade card falls short. That keeps your recipe stable once it is locked, instead of forcing your team to adjust the dose every time a new pigment lot arrives.
You can see the full range on our footwear manufacturing page.
If colour rejection is cutting into your output, talk to us about reducing colour rejection or request colour matching on your own sample. Bring one approved batch and one rejected batch, and we can work back from there.
FAQs
What causes colour rejection in footwear production?
Colour rejection usually comes from pigment lot variation, dosing or mixing errors, and mould-temperature or substrate differences between runs.
How do I reduce colour rejection on my production line?
Standardise your pigment and dosing, control mixing, inspect under a consistent light booth, and re-match every batch to an approved standard.
Does pigment quality affect the colour rejection rate?
Yes, since pigment that varies in strength or dispersion between lots shifts the shade even when your process stays the same, pushing rejections up.
How can a footwear colour manufacturer help cut rejection?
A good footwear colour manufacturer supplies consistent pigment lots and matches shades in-house, so your colour stays stable and fewer pairs are rejected.
What is an acceptable colour rejection rate in footwear?
There is no single standard, but strong units aim for low single-digit percentages, with the real goal being a steady, measurable rate you can trace and reduce.
How do you measure colour consistency?
Colour is measured with a spectrophotometer as Delta E, the difference from your target shade, where a lower Delta E means a closer, more consistent match.
Why choose Mittal Chemplast for footwear colour?
Mittal Chemplast has been a footwear colour manufacturer since 1982, offering the Ansh PU colourant range with in-house colour matching and consistent lot-to-lot shades.